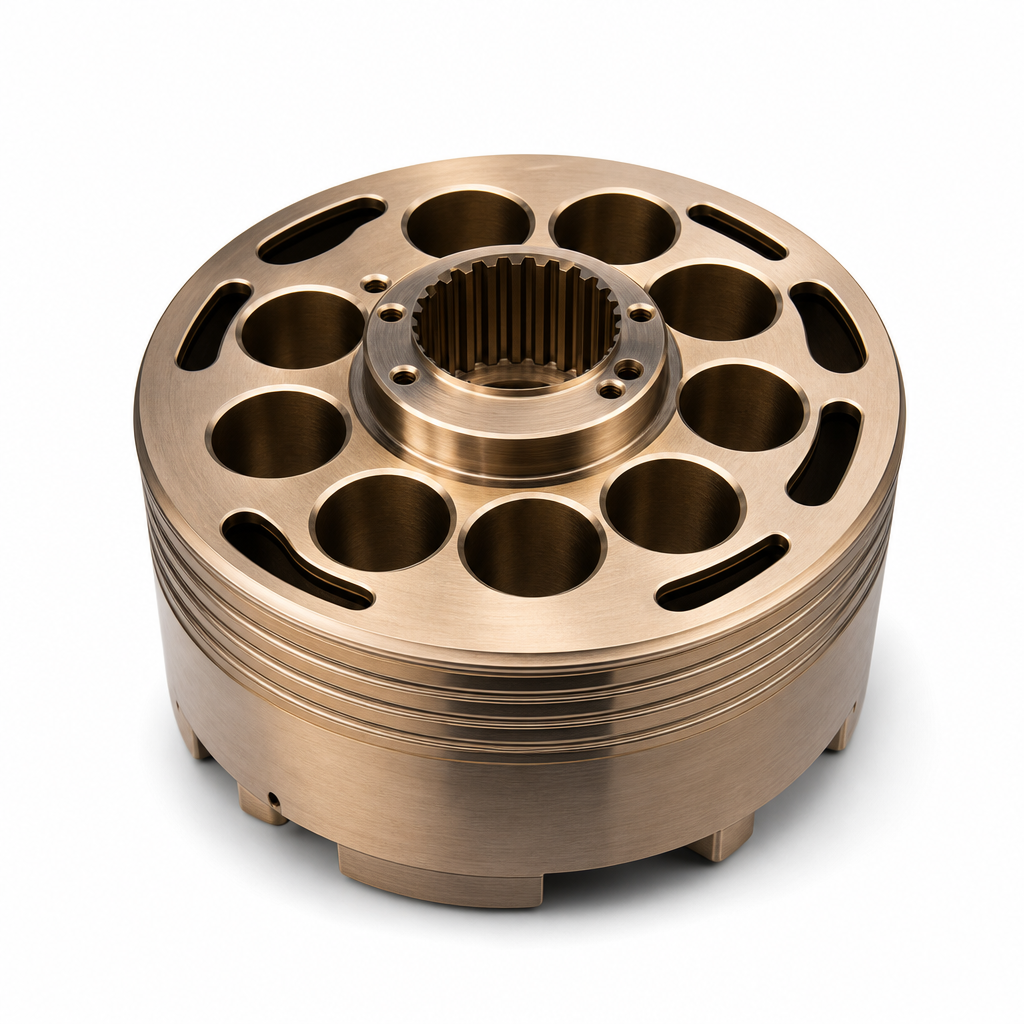
A bronze cylinder block for piston pumps, where the ten piston bores, the central spline bore and the port windows all share one datum. This is the copper-alloy part we build most for hydraulic pump and motor customers.
What a cylinder block decides is internal leakage and service life, and that comes down to three numbers: bore indexing, bore-to-valve-face perpendicularity, and valve face flatness. Miss the indexing and the pistons wear on one side; let the face collapse a few microns and pressure will not build while temperature climbs. So the ten bores are indexed to ±0.02 mm and held at H7, perpendicularity to the valve face is 0.01 mm, and the face is lapped separately to 0.005 mm flatness at Ra 0.4 µm. Bronze grabs the tool and deflects easily, so thin-wall sections are roughed and finished in two passes and cutting data is set per heat.
Send the displacement, rated pressure, bore count and material requirement — tin bronze, aluminium bronze or steel with a bronze liner. We will confirm the blank form, broaching and lapping allowance, then quote with CMM, roundness and lapping records. Reply within 48 hours.