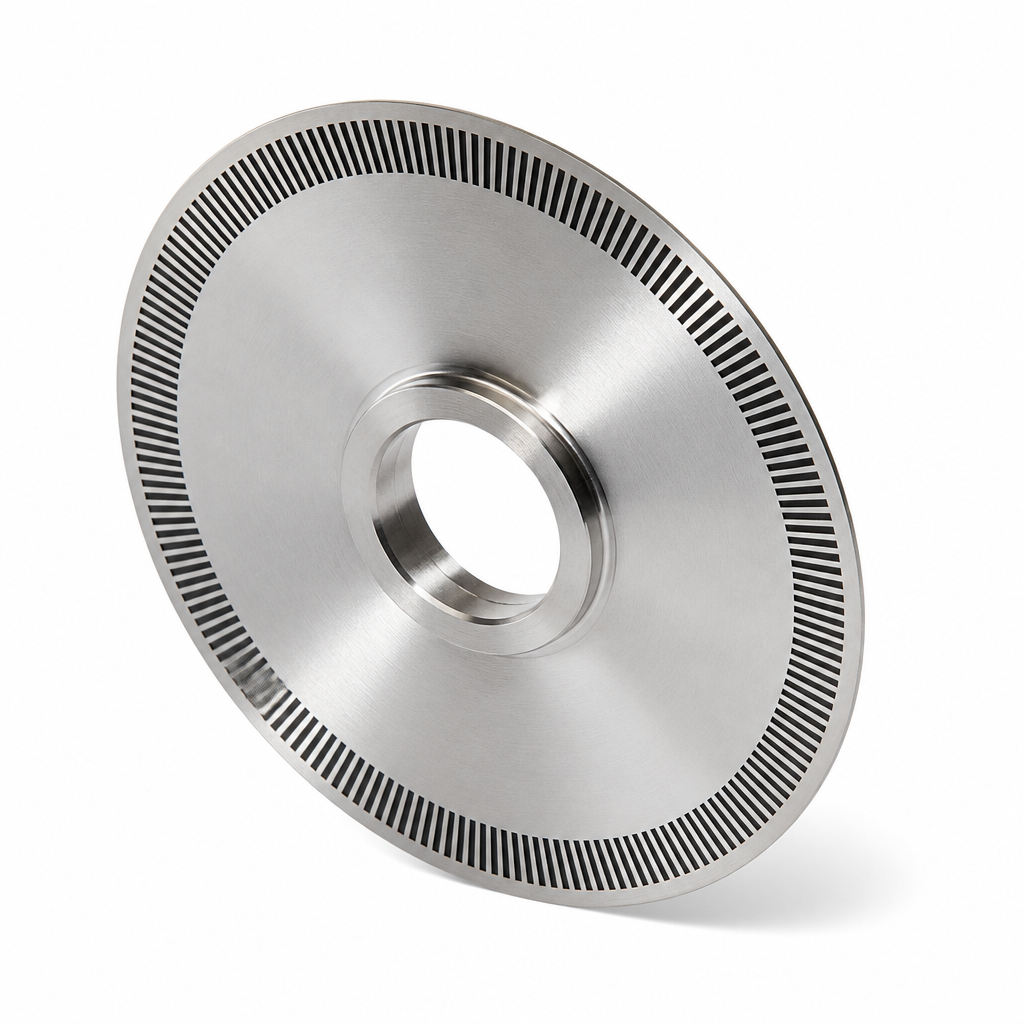
A radially slotted disc, faced on the lathe with a ring of narrow slots indexed around the rim. This is the thin-disc pattern we build most for drive, braking and heat-dissipation customers.
A thin disc really only has two hard points: flatness and the slots. A Ø300 disc warps as soon as the clamping force is uneven, so it is roughed, released and stress-relieved before finish turning — that is how 0.03 mm flatness and 0.05 mm runout hold. The slot band is milled on an indexer to ±0.02 mm width with ±0.05 mm cumulative index, and the slot edges are deburred as a separate step: a burr of even 0.05 mm will score the mating face, generate heat and noise, and the part gets blamed for it.
Send the outer diameter, thickness, slot count and width, flatness requirement and working speed. For thin parts we confirm the clamping and stress-relief plan first, then quote with flatness, slot and material reports. Reply within 48 hours.