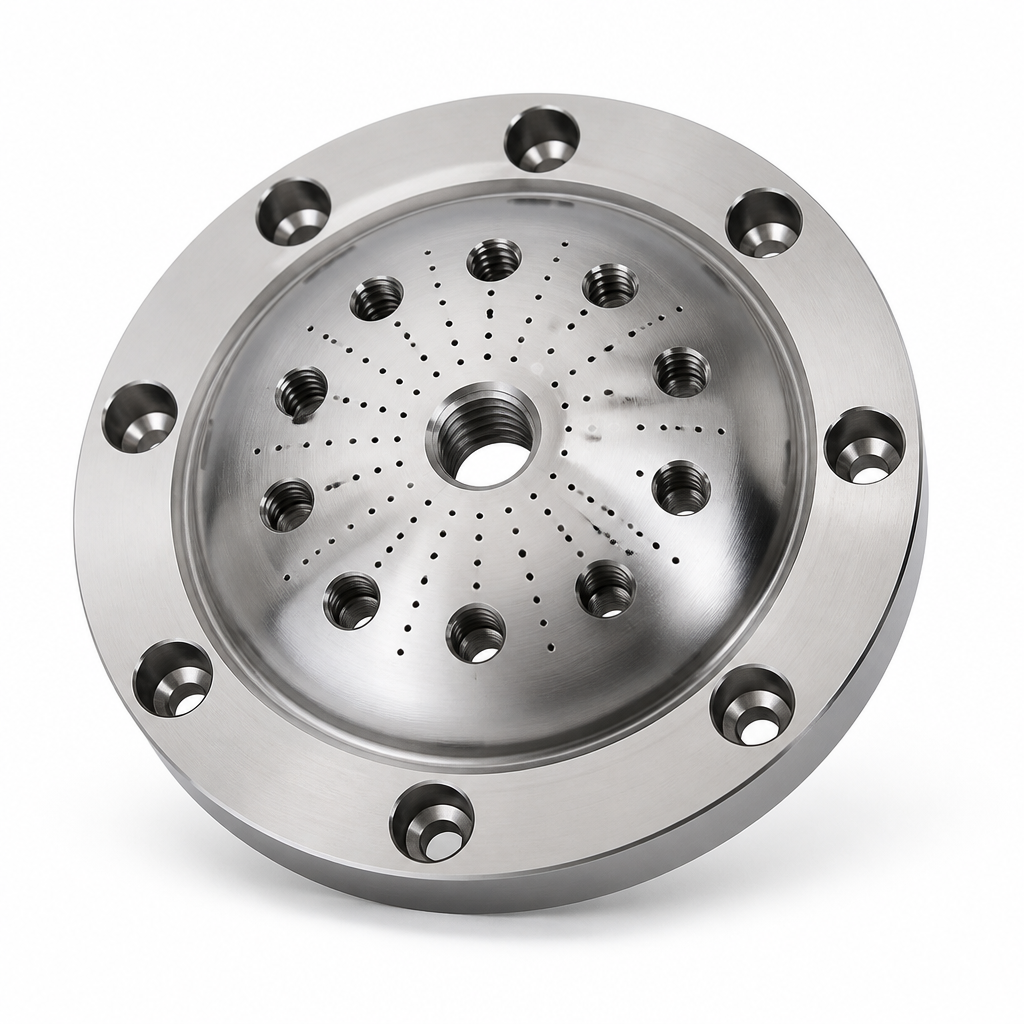
A port flange plate where the flange face, the recessed face, the outer counterbores and the inner tapped holes are all machined from one datum. This is the plate pattern we build most for vacuum and pneumatic distribution, fixturing and machine mounting faces.
What matters here is not the outline but two hole patterns and one face. The outer counterbores are drilled on PCD ±0.1 mm at a consistent depth, so the bolt heads seat flat; the inner tapped holes sit within ±0.05 mm and the centre thread is concentric to the spigot within Ø0.03 mm, so fittings screw down without binding; and the flange face is held to 0.02 mm flatness, which is what actually seals. The dozens of small holes in the face get a separate deburring step and an ultrasonic clean — chips left in those holes become throttling and contamination in a vacuum or air circuit, and the symptom shows up as low pressure or a workpiece that will not hold.
Send the interface — thread sizes, hole layout or assembly drawing — plus medium, pressure, and flatness and cleanliness requirements. We confirm the drilling sequence and cleaning process, then quote with CMM, thread gauge and cleanliness records. Reply within 48 hours.