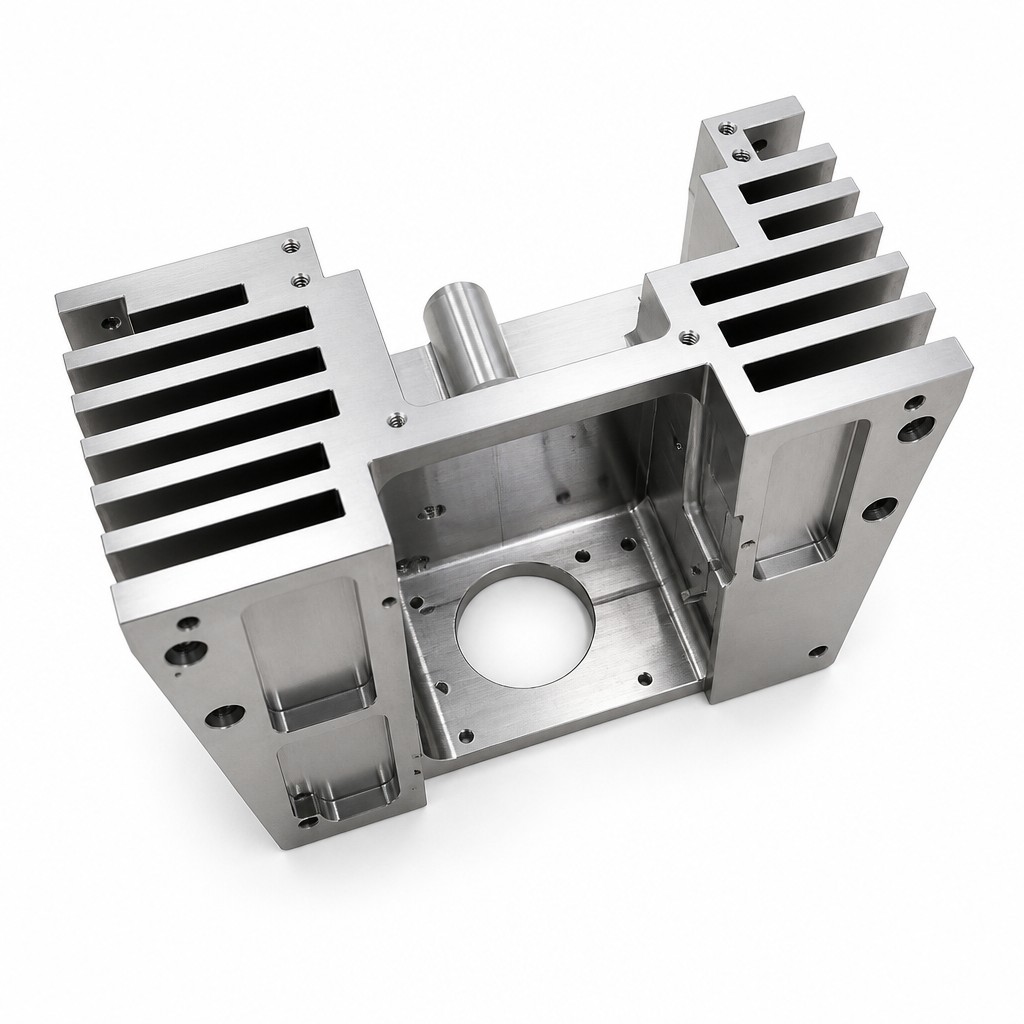
Mounting faces, internal cavity and the cooling fins on both sides are cut from one aluminium block; the deep cavity is roughed and finished in layers and the fin slots are stepped down to avoid thin-wall distortion.
The centre through-bore and the surrounding mounting holes are machined in the same operation, so the housing takes a motor or module directly.